Views: 0 Author: Site Editor Publish Time: 2026-10-19 Origin: Site
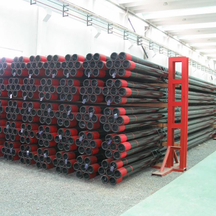
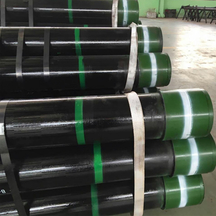
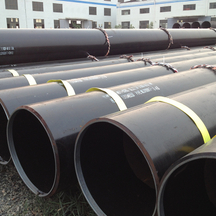
Straight seam high-frequency welded pipe (ERW) is produced by forming steel strip into a tube and joining the edges with high-frequency resistance welding. The process includes uncoiling, leveling, roll forming, welding, sizing, cutting, and inspection. ERW pipes offer efficient continuous production, consistent dimensions, and cost-effective manufacturing. They are widely used in construction, water supply, mechanical applications, and certain oil and gas transportation systems. Pipe quality depends on raw materials, edge preparation, welding control, forming accuracy, and final inspection.
Raw Material Preparation and Steel Strip Uncoiling
Raw material preparation and uncoiling are the first stages in straight seam high-frequency welded (ERW) pipe production. Steel strip quality directly affects forming stability, welding performance, dimensional accuracy, and finished pipe reliability. Manufacturers must carefully inspect incoming materials and ensure a stable strip supply.
Process Overview
Stage | What Happens | Key Point |
|---|---|---|
Raw material selection | Hot-rolled steel coils chosen by grade, composition, width, and thickness | Must meet application and standard (ASTM, API, EN) |
Incoming inspection | Verify material ID, dimensions, surface, traceability | Prevents unsuitable material entering production |
Uncoiling | Coil loaded on uncoiler; strip fed at controlled speed | Stable feeding prevents leveling/forming/welding issues |
Strip end joining | Current strip end welded to next coil start | Enables continuous production |
Accumulation | Accumulator stores strip reserve during coil changes | Capacity must match line requirements |
1. Raw Material Selection
ERW pipes are commonly made from hot-rolled steel coils. Steel grade, chemical composition, strip width, and thickness must meet application and standard requirements (ASTM, API, EN).
Different applications need different properties—structural pipes need strength and formability; fluid transportation pipes must meet pressure-service and material performance requirements. Correct grade selection reduces defects and ensures service suitability.
2. Incoming Steel Coil Inspection
Inspection Item | Purpose |
|---|---|
Material identification | Confirm grade, coil number, and certificates |
Thickness & width | Verify strip dimensions meet production requirements |
Surface condition | Identify rust, scratches, scale, cracks, or defects |
Material traceability | Record coil info for quality tracking |
Where required, verify chemical composition and mechanical properties via test certificates or additional testing. Proper inspection keeps unsuitable material off the line.
3. Steel Strip Uncoiling
The coil is loaded onto an uncoiler, which releases strip and feeds it into the line at controlled speed. Stable uncoiling matters—uneven feeding or excessive tension affects leveling, forming, and welding. Ensure the coil is securely positioned and the strip enters smoothly. Automated equipment helps maintain consistent feeding and reduces interruptions.
4. Strip End Joining and Accumulation
To support continuous production, the end of the current strip is welded to the start of the next coil. Ends may be trimmed first to remove irregular edges.
An accumulator stores a strip reserve, maintaining continuous operation while a new coil is loaded. Its capacity and speed must match line requirements.
5. Why This Stage Matters
Proper preparation and uncoiling establish the foundation for stable ERW pipe manufacturing. Incorrect material selection, damaged surfaces, inconsistent thickness, or unstable feeding can cause forming problems and welding defects later.
By combining material verification, dimensional checks, controlled uncoiling, and reliable strip joining, manufacturers improve efficiency and maintain consistent quality. These steps prepare the strip for leveling, edge preparation, and roll forming.
Steel Strip Leveling, Edge Preparation, and Forming
Leveling, edge preparation, and roll forming are essential stages in straight seam high-frequency welded (ERW) pipe production. After uncoiling, the strip must be prepared and shaped into a tubular form before welding. Accurate control ensures stable welding, consistent dimensions, and reliable quality.
Process Overview
Stage | What Happens | Key Point |
|---|---|---|
Leveling | Strip passes through rollers to flatten coil curvature | Improves flatness and feeding stability |
Edge preparation | Trimming, deburring, cleaning contaminants | Ensures suitable edges for welding |
Roll forming | Progressive rolls bend flat strip into open tube | Multiple stands; edges move toward welding position |
Edge alignment | Strip edges aligned before welding station | Consistent positioning for continuous weld seam |
1. Steel Strip Leveling
Steel coils retain curvature from storage and transport. A leveling machine with a series of rollers gradually flattens the strip, reducing coil curvature and improving flatness. This supports stable movement through the line and reduces uneven forming and dimensional deviations.
Particularly important for ERW pipes with tight tolerances or thin walls.
2. Steel Strip Edge Preparation
Edge preparation makes both strip sides suitable for high-frequency welding. Depending on material and requirements, this may include:
Edge trimming
Burr removal
Cleaning of contaminants
Edges must have suitable straightness and alignment. Uneven or damaged edges cause inconsistent contact during welding—increasing the risk of incomplete fusion or irregular weld seams. Contaminants and excessive scale near edges can also interfere with stable welding.
Carefully control strip width and edge condition to maintain consistent welding performance.
3. Roll Forming: Shaping the Strip into a Tube
After leveling and edge preparation, the strip enters the roll-forming section. A series of forming rolls gradually bends the flat strip into an open tubular shape through progressive deformation across multiple roll stands—not in a single operation.
During forming, strip edges move closer together until they reach the required position for welding. Rolls must be correctly aligned to maintain consistent geometry and prevent excessive deformation.
Forming Factor | Influence |
|---|---|
Strip width | Affects edge positioning |
Material thickness | Affects deformation behavior |
Roll design | Determines forming geometry |
Equipment alignment | Prevents edge misalignment |
Production speed | Affects forming stability |
Poor forming control may cause edge misalignment, excessive residual stress, or diameter variations—affecting weld quality and sizing operations.
4. Edge Alignment and Dimensional Control
Before the high-frequency welding station, the two strip edges must be accurately aligned. Consistent edge positioning establishes suitable welding conditions and supports a continuous longitudinal weld seam.
Operators monitor strip position, forming stability, and edge gap. Automated sensors and adjustment systems may detect deviations and maintain stable conditions.
5. Why Leveling and Forming Quality Matter
Leveling, edge preparation, and roll forming directly influence final ERW pipe quality. Accurate preparation improves welding stability, reduces material waste, and maintains specified OD and wall thickness.
By controlling strip flatness, edge condition, forming geometry, and alignment, manufacturers establish the conditions for reliable high-frequency welding. Once formed into an open tube with properly aligned edges, the strip is ready for high-frequency welding and weld seam formation.
High-Frequency Welding: The Core of ERW Pipe Production
High-frequency welding is the most critical stage in straight seam high-frequency welded (ERW) pipe production. The formed strip edges are heated by high-frequency current and pressed together to create a continuous longitudinal weld seam. Weld quality directly affects structural integrity, mechanical properties, and application suitability.
Unlike fusion welding with filler metal, conventional ERW joins heated edges through pressure without filler material. Accurate control of heating and squeezing is essential.
Process Overview
Stage | What Happens | Key Point |
|---|---|---|
Edge heating | High-frequency current concentrates near strip edges | Skin/proximity effect enables rapid, localized heating |
Squeeze-roll welding | Heated edges pressed together to form weld seam | Pressure and alignment control weld integrity |
Weld bead removal | Excess internal/external metal removed where required | Accurate removal maintains wall thickness and profile |
Parameter control | Power, speed, pressure, edge prep, alignment monitored | Prevents defects and ensures consistency |
1. High-Frequency Current and Edge Heating
After roll forming, the open tube enters the welding station. A high-frequency power supply delivers current to adjacent strip edges via induction or contact systems.
Current concentrates near the edges due to skin and proximity effects—heating them rapidly while limiting surrounding heating. Temperature and distribution depend on:
Welding power
Current frequency
Line speed
Material thickness
Edge geometry
Stable heating is essential. Insufficient heat → incomplete bonding; excessive/uneven heat → weld irregularities and defects.
2. Squeeze-Roll Welding
When edges reach welding temperature, squeeze rolls apply pressure to bring them together and form a continuous seam. Molten or highly heated material and surface oxides may be expelled, depending on conditions. The weld must have sufficient continuity and integrity.
Control carefully:
Welding pressure
Edge alignment
Squeeze-roll position
Inconsistent pressure or poor alignment can cause incomplete fusion, irregular weld formation, or excessive beads.
3. Weld Bead Removal
Excess metal may remain inside and outside the seam. Where required, specialized tools remove beads to achieve specified profiles.
Removal Issue | Consequence |
|---|---|
Excessive removal | Reduces local wall thickness |
Insufficient removal | Leaves protrusions affecting processing or service |
Finished weld profile must comply with dimensional and quality specifications.
4. Welding Parameter Control and Defect Prevention
Parameter | Requirement |
|---|---|
Welding power | Sufficient energy for proper edge heating |
Production speed | Compatible with heating conditions |
Squeeze pressure | Effective bonding between heated edges |
Edge preparation | Clean, properly aligned edges |
Equipment alignment | Consistent seam formation |
Common defects: incomplete fusion, cracks, inclusions, seam discontinuities. Prevent through process monitoring, equipment maintenance, and qualified inspection.
5. Why High-Frequency Welding Quality Matters
A reliable longitudinal weld seam is essential for ERW pipe performance. Even with compliant base material, poor welding control can compromise the finished product. Manufacturers must maintain stable conditions and verify weld integrity through inspection per the applicable standard.
After welding and bead removal, the pipe proceeds to heat treatment (if specified), sizing, straightening, and cutting to achieve final dimensions and characteristics.
Post-Weld Treatment, Sizing, and Pipe Cutting
After high-frequency welding, ERW steel pipes undergo finishing operations to achieve required mechanical properties, dimensional accuracy, and product specifications. These may include post-weld heat treatment, cooling, sizing, straightening, cutting, and end finishing. The process depends on steel grade, dimensions, manufacturing requirements, and applicable standards.
Finishing Operations at a Glance
Operation | Purpose | Key Point |
|---|---|---|
Post-weld heat treatment | Improve weld-zone properties; reduce welding effects | May be localized or full-pipe; depends on grade and standard |
Cooling & temperature control | Maintain dimensional stability before sizing | Controlled cooling prevents deformation |
Sizing | Control final OD, roundness, and ovality | Precise roll alignment essential |
Straightening | Correct longitudinal bending | Important for structural and mechanical applications |
Cutting | Cut continuous pipe to specified lengths | Flying saws or automatic systems; maintain length tolerance |
End finishing | Deburring, facing, beveling, threading | Per application and purchase specification |
Surface preparation | Cleaning, coating, finishing | Per service environment and specification |
1. Post-Weld Heat Treatment
High-frequency welding creates rapid, localized heating and cooling—causing microstructure and property differences between weld zone and base material. When required, post-weld heat treatment improves weld-region properties. It may be localized (weld seam) or full-pipe, depending on grade, application, and standard.
Not every ERW pipe needs the same treatment. Control heating temperature, treatment time, and cooling conditions to achieve results without compromising the base material.
2. Cooling and Temperature Control
After welding or heat treatment, the pipe must cool under controlled conditions before further processing. Proper temperature management maintains dimensional stability and reduces deformation risk during sizing. Excessive or uneven temperature changes can cause dimensional variation or unwanted property changes. Monitor pipe temperature before the next stage.
3. Sizing and Straightening
Sizing: The welded pipe passes through sizing rolls that adjust dimensions to meet tolerances—correcting OD variation, roundness, and ovality. Precise roll alignment and stable production conditions are essential for dimensional accuracy.
Straightening: Corrects longitudinal bending and improves overall straightness. Particularly important for structural pipes, mechanical applications, and piping systems requiring accurate dimensions for installation.
4. Pipe Cutting to Specified Lengths
The continuous pipe is cut into individual lengths using flying saws or automatic cutting systems synchronized with production speed. Cutting accuracy affects usability, packaging, and installation. Ensure each pipe meets length tolerance and cutting does not cause excessive deformation or end damage. Standard and customized lengths may be available.
5. End Finishing and Surface Preparation
After cutting, pipe ends may undergo:
Deburring
End facing
Beveling (for welded connections)
Threading (when specified)
Surface cleaning, protective coating, or other finishing may be performed per service environment and purchase specification.
6. Importance of Finishing Operations
Post-weld treatment, sizing, and cutting transform continuously welded tubing into finished products. Effective temperature control supports stability; accurate sizing and cutting ensure consistent dimensions and easier installation.
By controlling each stage, manufacturers reduce dimensional deviations, improve efficiency, and prepare pipes for final inspection—where dimensions, surface condition, weld integrity, and specified properties are checked before delivery.
Finished ERW Pipe Inspection and Quality Control
Finished product inspection is the final critical stage in ERW pipe production. After welding, sizing, straightening, and cutting, each pipe must be checked to verify dimensional tolerances, material properties, and product standards. Effective inspection identifies defects, reduces failures, and ensures application suitability.
Inspection requirements depend on steel grade, dimensions, applicable standards, and purchase specifications. A quality control system should cover material traceability, production records, inspection results, and final acceptance.
Inspection Checklist at a Glance
Inspection Type | What to Check |
|---|---|
Visual | Surface, weld seam, pipe ends—cracks, dents, scratches, corrosion, irregular weld profile |
Dimensional | OD, wall thickness, length, ovality/roundness, straightness, end condition |
Weld seam NDT | Ultrasonic or eddy-current testing for weld discontinuities |
Mechanical | Tensile, flattening, bend, or other applicable tests |
Hydrostatic | Leakage or failure under specified test pressure (pressure service) |
Traceability | Material grade verification, mill certificates, markings, records |
1. Visual Inspection
First check on finished pipes. Inspectors examine the external surface, weld seam, and pipe ends for cracks, dents, scratches, corrosion, and irregular weld profiles. Also verify weld bead removal and end finishing meet requirements. Any visible defect affecting performance or violating acceptance criteria must be evaluated before approval.
2. Dimensional Inspection
Item | Check |
|---|---|
Outside diameter | Meets specified tolerance |
Wall thickness | Verified at appropriate locations |
Length | Matches purchase specification |
Ovality/roundness | Cross-section maintains required shape |
Straightness | Does not exceed permitted bending deviation |
End condition | Squareness, bevel dimensions, threading (if applicable) |
Measuring instruments must suit required tolerances and be properly maintained.
3. Weld Seam Nondestructive Testing (NDT)
ERW pipes rely on a longitudinal welded joint, so weld inspection is critical.
Method | Principle |
|---|---|
Ultrasonic testing | Sound waves detect internal or weld-related discontinuities |
Eddy-current testing | Electromagnetic principles identify certain near-zone defects |
Method and coverage depend on product standard and purchase requirements. NDT helps identify potential weld defects but does not replace other required inspections or guarantee zero defects.
4. Mechanical and Hydrostatic Testing
Mechanical testing evaluates performance—may include tensile, flattening, bend, or other applicable tests, assessing strength, ductility, and deformation resistance.
Hydrostatic testing may be required for pressure service. The pipe is filled with water and subjected to specified test pressure for the required period. Inspectors check for leakage or failure signs per acceptance criteria.
Not every ERW pipe requires every test. Follow the governing standard and agreed purchase specification.
5. Material Verification and Traceability
Manufacturers verify grades and maintain records linking finished pipes to original steel coils and production batches. Chemical composition and mechanical properties may be confirmed through mill test certificates and additional testing.
Product markings, inspection records, and material certificates help buyers confirm identity and compliance. Traceability is especially important for industrial piping, infrastructure, and strict-quality applications.
6. Final Acceptance and Quality Documentation
Before shipment, finished pipes undergo a final review of inspection results, markings, quantities, and packaging. Nonconforming products are identified and handled per quality procedures.
Documentation may include:
Mill test certificates
Dimensional inspection records
NDT reports
Hydrostatic test results
Other required quality documents
Conclusion
Straight seam high-frequency welded pipe (ERW) production converts steel coils into reliable finished pipes through controlled forming, welding, sizing, cutting, and inspection. Accurate edge alignment and stable high-frequency welding help ensure consistent weld quality, while post-weld treatment may be applied when required. Quality control should cover raw materials, welding parameters, dimensional accuracy, nondestructive testing, mechanical testing, and hydrostatic testing, in line with applicable standards such as ASTM A53 or API 5L. For buyers, selecting the right ERW pipe means confirming steel grade, outside diameter, wall thickness, length, standard, inspection requirements, and service conditions, and verifying material certificates and inspection reports.
FAQ:
Q1: What are the main steps in the production process of straight seam high-frequency welded pipe (ERW)?
The main steps include steel coil inspection and uncoiling, strip leveling, edge preparation, roll forming, high-frequency welding, weld bead removal, optional heat treatment, sizing, cutting, and finished product inspection.
Q2: How does high-frequency welding work in ERW steel pipe manufacturing?
High-frequency current rapidly heats the edges of the formed steel strip, and squeeze rolls press the heated edges together to create a continuous longitudinal weld seam.
Q3: What inspections are required for finished ERW steel pipes?
Depending on the applicable standard and purchase specification, inspections may include visual and dimensional checks, weld seam nondestructive testing, mechanical tests, hydrostatic testing, and verification of material documentation.
Q4: What is the difference between ERW steel pipe and seamless steel pipe?
ERW steel pipe is manufactured by forming steel strip and welding its edges, while seamless steel pipe is produced from a solid billet without a longitudinal weld seam. The appropriate choice depends on the required specifications, service conditions, and project requirements.
Q5: Which factors most affect the quality of high-frequency welded steel pipes?
Raw material quality, strip edge preparation, welding power and pressure, forming accuracy, process stability, and final inspection all influence ERW pipe quality.
About Us / News / Product / Project / Quality Assurance / Service / Contact Us